TL;DR — Quick Answer
Choose your toolholder based on your primary application. For most modern machining: choose HSK-63A for metalworking and heavy milling where torque is prioritized, and HSK-63F for woodworking, composites, or soft metals where high-speed matters most.
Read on for the full breakdown, comparison tables, and specific recommendations.
Choosing the right toolholder for your application
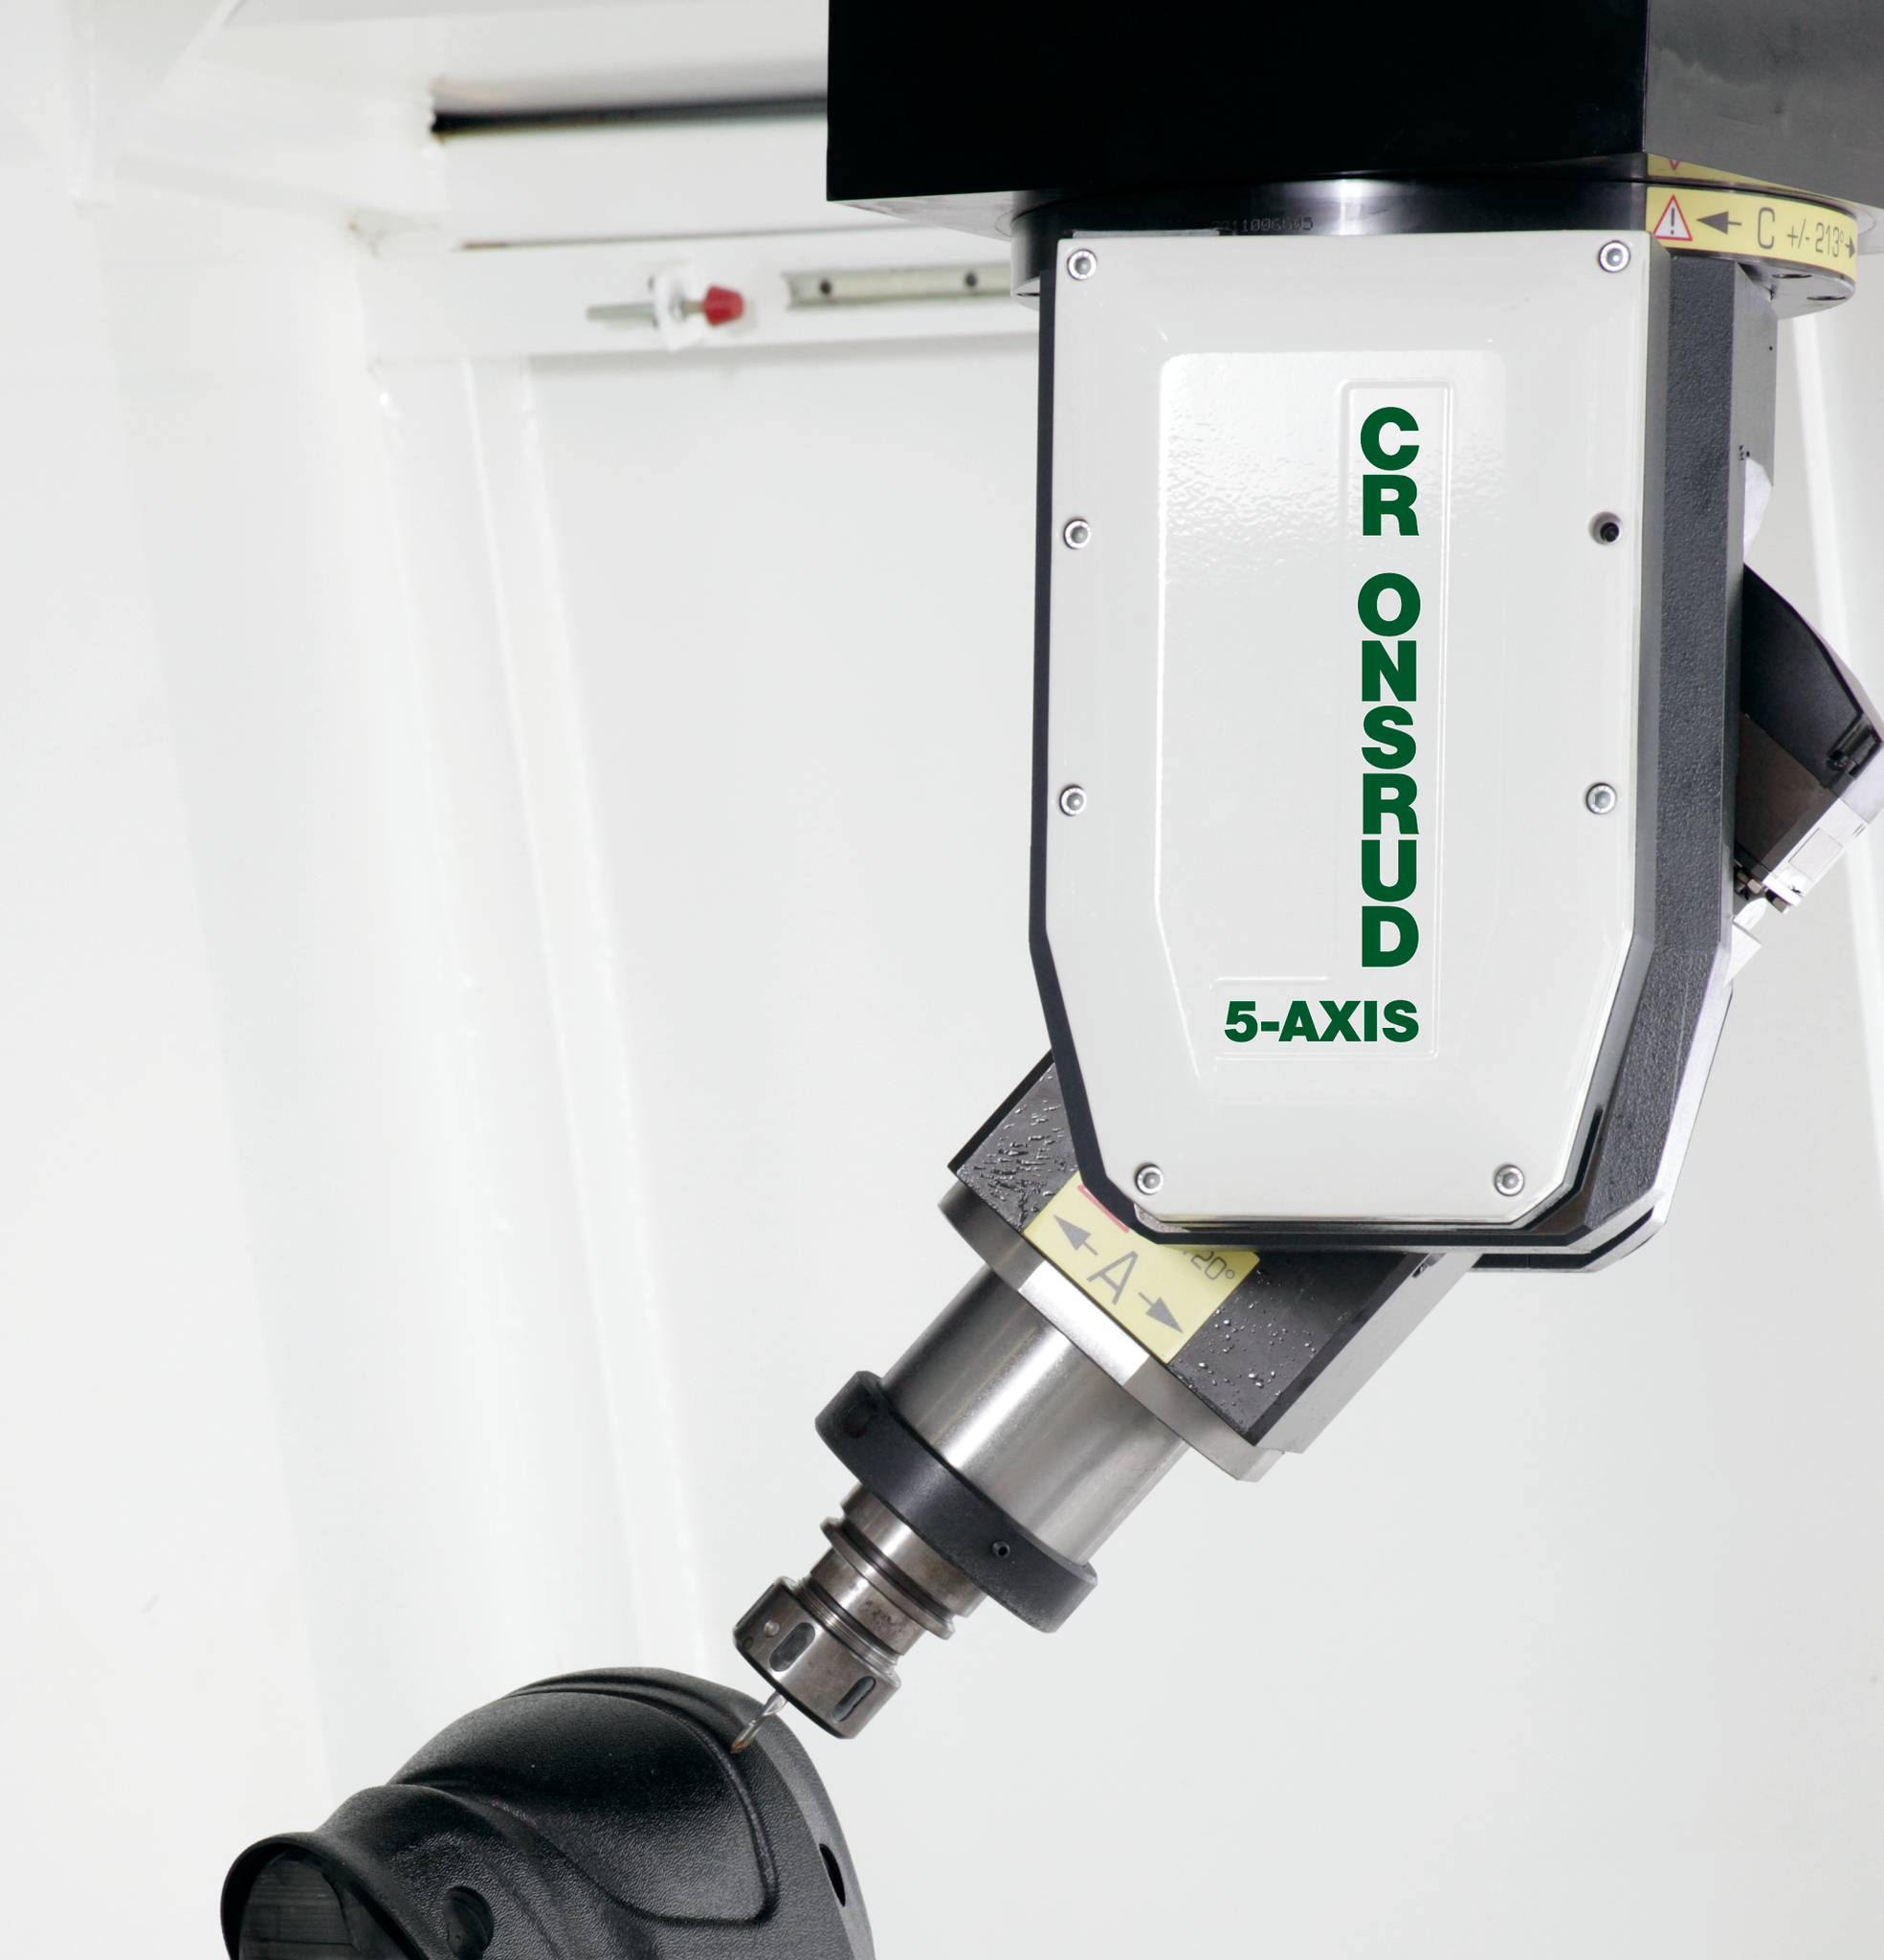
For high-speed CNC machining, machinists often use HSK (Hollow Taper Shank) toolholders. The hollow style provides less mass than many other toolholders, so the HSK can spin at higher speeds and perform faster tool changes.
The dual-contact design simultaneously secures the tool against both the internal spindle taper and the flange (or outer spindle face), which dampens the vibrations that are the primary cause of chatter in precision machining. It also prevents the uneven thermal expansion between the spindle taper and the tool holder, ensuring highly accurate cutting depths. In addition, this dual contact prevents fretting, a common issue where standard tapers progressive wear down the spindle wall.
- Minimal Deflection: Provides resistance when processing hard materials or performing heavy-duty operations.
- Dampened Vibrations: Produces a smooth surface finish during high-speed or deep-pocket cutting.
- Accuracy: Decreases runout deviation both radially and axially and ensures consistency during automatic tool changes.
- High Speed: Centrifugal force expands the hollow shank taper outward, locking it tightly against the spindle to maintain stability at high rpm (unlike BT, CAT, and ISO).
- Increased Tool Life: Minimizes cutting edge wear, preserving tools over long production runs.
The most used styles for high-speed CNC machines are the HSK-63A and HSK-63F. While they share the core benefits of the HSK style, key differences make each ideal for different applications.
| HSK-63A | HSK-63F | |
|---|---|---|
|
Application |
General purpose milling, boring, and drilling; medium to heavy-duty metalwork; complex profiling | Woodworking; nested-based machining; plastic; composites; soft metals |
|
Design |
Shank has drive slots*; flange has both slots and keyways | Symmetrically round; relies on friction against the spindle taper for torque |
|
Torque |
Moderate to High | Medium |
|
Speeds |
15,000 to 20,000rpm | Up to 24,000rpm |
|
Flange Diameter |
63mm | 63mm |
|
Core Diameter |
48mm | 38mm |
|
Shank Length |
32mm |
24mm |
|
Internal Taper Size |
63mm | 50mm |
|
* Drive slots provide a physical connection that prevents the toolholder from slipping or spinning within the spindle. The slots are asymmetrical, so the toolholder can only be loaded in a specific orientation. This helps with applications that need tool orientation (e.g., rigid tapping). |
||
What About Other HSK Options?
HSK-63A and HSK-63F are the preferred standards in the HSK line for modern high-speed CNC machining. Although there are other HSK styles, they are outdated or used for niche purpose:
HSK-B: Largely considered obsolete for high-speed machining, its large flange diameter created balancing challenges, making it a poor choice for modern high-speed CNC operations.
HSK-C and HSK-D: Designed for manual clamping, they are unable to take advantage of automatic tool changers (ATC) on modern CNC machines.
HSK-E: Engineered for very specific lightweight applications that require extreme speeds (e.g., mold/die finishing at 40,000rpm), it lacks the rigidity necessary for standard or aggressive machining.
HSK-T: Features tighter keyway tolerances engineered specifically for lathe turning applications.
Why Other Toolholders May Not Be As Beneficial
Toolholders, such as the BT ,CAT, and ISO, were the industry standard for decades. As spindle speeds increased and the industry shifted to more complex (e.g., 5-axis) and higher rpm work, these legacy styles fell short. With only one contact point between the toolholder and the spindle, there is quite a bit of runout, where the tool is spinning off-center (i.e., wobbles). This imbalance causes uneven tool wear, premature wear, and breakage, especially at higher rpm. Additionally, over prolonged use, the taper on the spindle and the tool holder expand at different rates, leading to depth-of-cut inaccuracies.
Other larger toolholders (e.g., BT50 and CAT50) have more mass but as a result operate much slower. These are designed for substantially heavy-duty, specific applications.
Frequently Asked Questions
Will the HSK-63A toolholder fit in an HSK-63F spindle or vice versa?
No. While their outer flange diameters are both 63mm, the HSK-63F taper is smaller than the HSK-63A. The taper must match the taper inside your machine’s high-speed spindle. Also the HSK-63A has drive slots and keyways that will not fit inside the HSK-63F spindle.
What toolholder maintenance is involved?
Daily: Inspect the toolholder to ensure the taper is not out of round, oversized, or damaged in any way, which can affect tool changes.
Also inspect your collet assembly where build up can lead to bit breakage or poor cut finishes. Clean with a rust-free solvent and lubricate properly. See Chips & TIps: Nut and Collet Cleaning for more details.
3+/- months: Replace collets and perform a full inspection for damage, wear, or corrosion. 3 months is based on 8 hours/daily and 40hr workweek. Step replacement up or down accordingly.
Am I limited in what tools I can use with an HSK-63A or HSK-63F toolholder?
No, the type of cutting tools you can use with an HSK-63A or HSK-63F are nearly limitless up to the maximum tool shank size of 30-32mm typically. Simply use adapters with your toolholder that match your spindle type. Both the HSK-63A and HSK-63F support a wide variety of toolholding accessories, such as: standard nut and collet assemblies, milling and hydraulic chucks, thermogrip or shrink fit holders, hydraulic press styles, and more. The only limitation is spindle compatibility. Learn more: Chips & Tips: Comparing Tool Holder Assemblies.
If you have tooling questions, reach out to our Tooling Team: https://onsrudtooling.com/contact-us/